Cooler Bag Printing: Why a Foam-Lined Bag Cannot Take the Heat Your Logo Needs
Here is the sentence that causes more cooler bag reprints than any other: “can we do the same full-colour print we did on the tote?” On a tote bag, that is a simple yes. On a cooler bag it is a question about physics, because a cooler bag is not a piece of fabric. It is a laminate — shell, foam, foil film, liner — and two of those layers start to deform at temperatures that a heat press reaches in seconds.
Dye sublimation, the method that gives you edge-to-edge colour on polyester, typically runs at around 196–204°C for 45–60 seconds. Polyethylene foam softens and collapses long before that. So the honest answer is not “no” — it is “yes, but only if we print the panel before the bag exists.” That single sequencing decision is what this article is about, and it is the thing most quotations never mention until the artwork is already approved.
The constraint that never makes it into a cooler bag quotation
Every decoration method applies energy to the surface: heat, pressure, ink solvent, or a needle. On a single-layer bag that energy has one thing to travel through. On an insulated bag it travels into a stack that includes a closed-cell foam and a metallised film, and each of those has a limit:
- The foam is the weak link. Polyethylene foams have limited heat resistance and deform under sustained heat and pressure — you get a permanent flat, shiny patch exactly the size of the platen.
- The foil laminate is bonded with adhesive. Enough heat travelling inwards and that bond releases, so the lining bubbles or peels away from the foam months later.
- Non-woven polypropylene shells have their own ceiling — the fabric itself softens and glazes well below sublimation temperature.
- The zip, piping and webbing sit right at the panel edges, and synthetic tape does not enjoy a hot platen either.
None of this makes cooler bags hard to brand. It just means the decision order is inverted compared with a tote. On a tote you choose artwork, then a method. On a cooler you choose the build, then the method, then the artwork. If you have not yet fixed the build, start with how the foam and foil layers actually hold temperature — the thickness you land on changes what the panel can take.
The temperature ladder: what each method needs versus what the build survives
This is the reference table we work from. The temperatures are the published operating windows for each decoration process; the last column is the production consequence on an insulated bag.
| Method | Typical heat / dwell | On an assembled cooler bag | Verdict |
|---|---|---|---|
| Dye sublimation (polyester) | ~196–204°C, 45–60 sec | Foam crushes, laminate can release | Panel-stage only, before lamination |
| Heat transfer vinyl | ~152–160°C, 10–15 sec (low-temp films ~132–143°C) | Workable with a low-temp film, light pressure, short dwell | Yes, with a tested setting |
| DTF transfer | ~160°C for 5–7 sec, then a ~132–138°C cure | Short dwell is the advantage — heat does not reach the foam | Best route for full colour |
| Silkscreen | Air or low-heat cure, no platen pressure | No thermal risk; needs a flat, firm panel to squeegee against | Safest for 1–3 spot colours |
| Embroidery | No heat — needle penetration | Perforates the wall; must be done at panel stage or on a patch | Yes, with planning |
| Woven label / rubber patch | Stitched on, no heat | Attached to a strap, pocket or seam rather than the insulated wall | Always available |
Print the panel, then build the bag
The rule that unlocks almost everything: decoration that would damage the finished bag is harmless on a flat piece of shell fabric before the foam is behind it. A full-sublimation cooler is made by printing the polyester roll, cutting the panels, then laminating and sewing. The heat never touches the foam because the foam is not there yet.
This has three practical consequences that belong in your planning, not in a surprise email later:
- Artwork locks earlier. Panel-stage printing sits at the front of the production sequence, so a late artwork change is not a late change — it is a restart. Approve early and the 21–45 day production window after artwork approval stays intact.
- Colour extends into the seams. Because you are printing flat stock, the design can bleed off the panel edge, wrap the gusset and continue onto the lid. Nothing else gives you that.
- Reprints are not cheap fixes. With surface methods you can re-press a bad bag. With panel-stage printing the bag has to be re-made from fabric up, which is exactly why we insist on a signed digital mockup first.
The question to ask any supplier
“Is my print going on the fabric before assembly, or onto the finished bag?” If a supplier quotes full-bleed sublimation on an assembled foam-lined cooler with a short lead time, something in that answer is not right — and you will find out at delivery.
Silkscreen on 600D, non-woven and laminated shells
For one to three solid spot colours, silkscreen remains the workhorse and it carries no thermal risk at all. What it does need is a panel the squeegee can work against. On a 6 mm foam-walled bag the front panel is soft and slightly domed, so we screen either at panel stage or with a backing board inserted into the compartment to give a firm bed. Ask for that detail; it is the difference between a crisp edge and a smudged one.
Shell fabric changes the result more than most buyers expect. On 600D polyester the ink sits on a tight, slightly shiny weave and holds fine detail well. On plain non-woven polypropylene the surface is porous and low-energy, so ink sits on top rather than soaking in and needs a heavier deposit. On a laminated non-woven — the glossy one that looks like it has been shrink-wrapped — the film face is smoother still and demands an ink system formulated to key onto it. On foil-faced foldable coolers, printing goes on the outer face only; nobody should be printing the food-contact side.
Heat transfer and DTF: the safe middle, and where it lifts
For photographic logos, gradients and multi-colour artwork on an already-assembled bag, DTF is usually the right answer. The reason is dwell time, not temperature: a first press of five to seven seconds followed by a lower-temperature cure puts far less total energy into the wall than a minute-long sublimation cycle. Low-temperature heat transfer films do the same job for cut-vinyl style artwork.
Where heat-applied graphics fail on cooler bags is at the edges, and almost always for the same reason: the transfer was placed too close to a seam, a zip line or a quilted channel, so part of it never received even pressure. That corner then becomes the first place a fingernail catches. It also becomes the first place moisture gets underneath, which is one more reason to understand why a printed panel lifts near a wet seam before you place the logo.
Embroidery through an insulated wall
Embroidery reads as premium and is a favourite for management gifts, but it involves thousands of needle penetrations through the panel. Put that straight through an assembled insulated wall and you have perforated the barrier that keeps meltwater out of the foam. There are two clean solutions. Embroider at panel stage, before the foam and liner go in, so the stitching only ever passes through the shell. Or embroider a separate patch or a front pocket and attach that to the bag — which also lets a stiff, dense logo sit on a stable base instead of puckering a soft foam wall.
Keep embroidered marks simple. Fine serifs, thin rules under about 1 mm and small reversed-out type do not survive at the stitch densities that a bag panel can take without distorting.
When the panel says no: the other branding surfaces
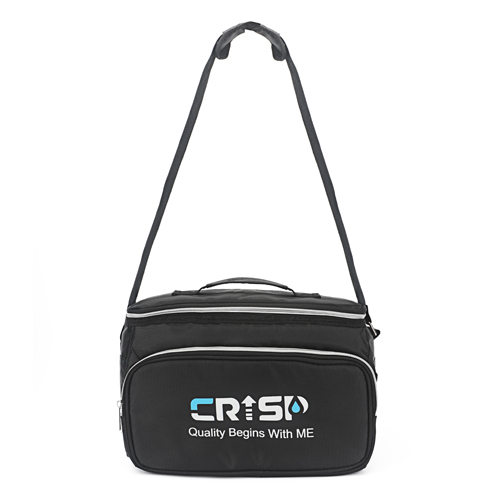
A cooler bag has more branding real estate than a tote, and the alternatives are often better looking. A woven label on the shoulder strap; a moulded or metal zip pull carrying the logo; contrast piping and webbing in brand colours; a printed front pocket panel; a branded lid flap. On a corporate gift these read as considered design rather than a sticker, and none of them puts heat anywhere near the foam. They also survive better, because a strap label never gets scrubbed the way a front panel does.
One caution: the size of your usable panel is set by the bag’s shape, not by your logo. A tall slim lunch cooler and a wide grocery tote of the same litreage present very different canvases, so settle the capacity brief that decides your print panel size before the design work starts.
The cooler bag print pre-flight checklist
- Build confirmed first: shell fabric, foam thickness, lining type — all three, in writing.
- Method chosen against the build, not against the artwork.
- Print stage stated on the order: panel-stage or finished-bag.
- Artwork supplied as vector (AI, EPS or PDF) with fonts outlined; raster only for DTF or sublimation, and then at full size.
- Keep at least 15 mm clear of every seam, zip tape, quilt line and gusset fold.
- Check the logo against the shell colour — a mid-grey or navy shell shifts every unsupported tint.
- Reversed-out type set no lighter than the shell will hold; add a keyline if in doubt.
- Second position decided (strap label, zip pull or pocket) — it usually costs less than enlarging the main print.
- Digital mockup approved and signed before production. The clock on the 21–45 day window starts there.
Work through those nine lines and the awkward conversations disappear. If you would rather have us do it with you, the cooler bag printing options we run in-house cover every method in the table above, and we will tell you plainly when your artwork needs a different one.
Frequently asked questions
Can you print a full-colour photographic logo on a cooler bag?
Yes. On an assembled bag, DTF handles full colour with a short press cycle. For edge-to-edge coverage across the whole bag, we sublimate the polyester at panel stage before the foam and lining are laminated in.
Why can’t you sublimate a finished insulated bag?
Sublimation needs roughly 196–204°C held for 45–60 seconds. Polyethylene foam deforms under that, and the adhesive bonding the foil laminate can release. You would get colour and a crushed, glazed panel.
Which printing method lasts longest on a cooler bag?
For everyday wet-and-wipe use, a well-cured silkscreen on 600D polyester and an embroidered patch both outlast heat-applied graphics, because neither has an edge that can lift. Panel-stage sublimation is effectively permanent since the dye is in the fibre.
How big can the logo be?
Indicatively, around 16–24 cm wide on a front panel, 12–16 cm on a lid and 8–12 cm on a side panel, with exact areas confirmed on your mockup. Full sublimation removes the limit entirely because the artwork is printed before the bag is cut.
What is the minimum order and turnaround?
From 300 pcs, with 21–45 days production after artwork approval plus around 15 days shipping. Express in 10 working days is possible on limited styles and quantities — usually surface decoration rather than panel-stage printing. Quote-only, SST invoiced, and ePerolehan documentation available.
Send the artwork, we will tell you what the build can take
Share your logo files, the bag style and the quantity, and you will get a free digital mockup with the recommended method, print positions and indicative sizes — usually within one business day. If the artwork needs a different method than you had in mind, we will say so before you approve, not after. Aquaholic Gifts is a Singapore-based corporate gifting specialist since 2003, now serving Malaysia from Kuala Lumpur.
Request a mockup for custom printed cooler bags and we will take it from there.
WhatsApp +60 10 717 5924 · Send your brief through our contact page
Aquaholic Gifts Malaysia — AS80, Jalan Hang Tuah 4, Taman Salak Selatan, 57100 Kuala Lumpur. MOQ from 300 pcs, delivered nationwide.